Increased Safety (Ex e) Motors Explained: Ex e vs Flameproof Ex d
Increased Safety (Ex e) Motors Explained: Ex e vs Flameproof Ex d
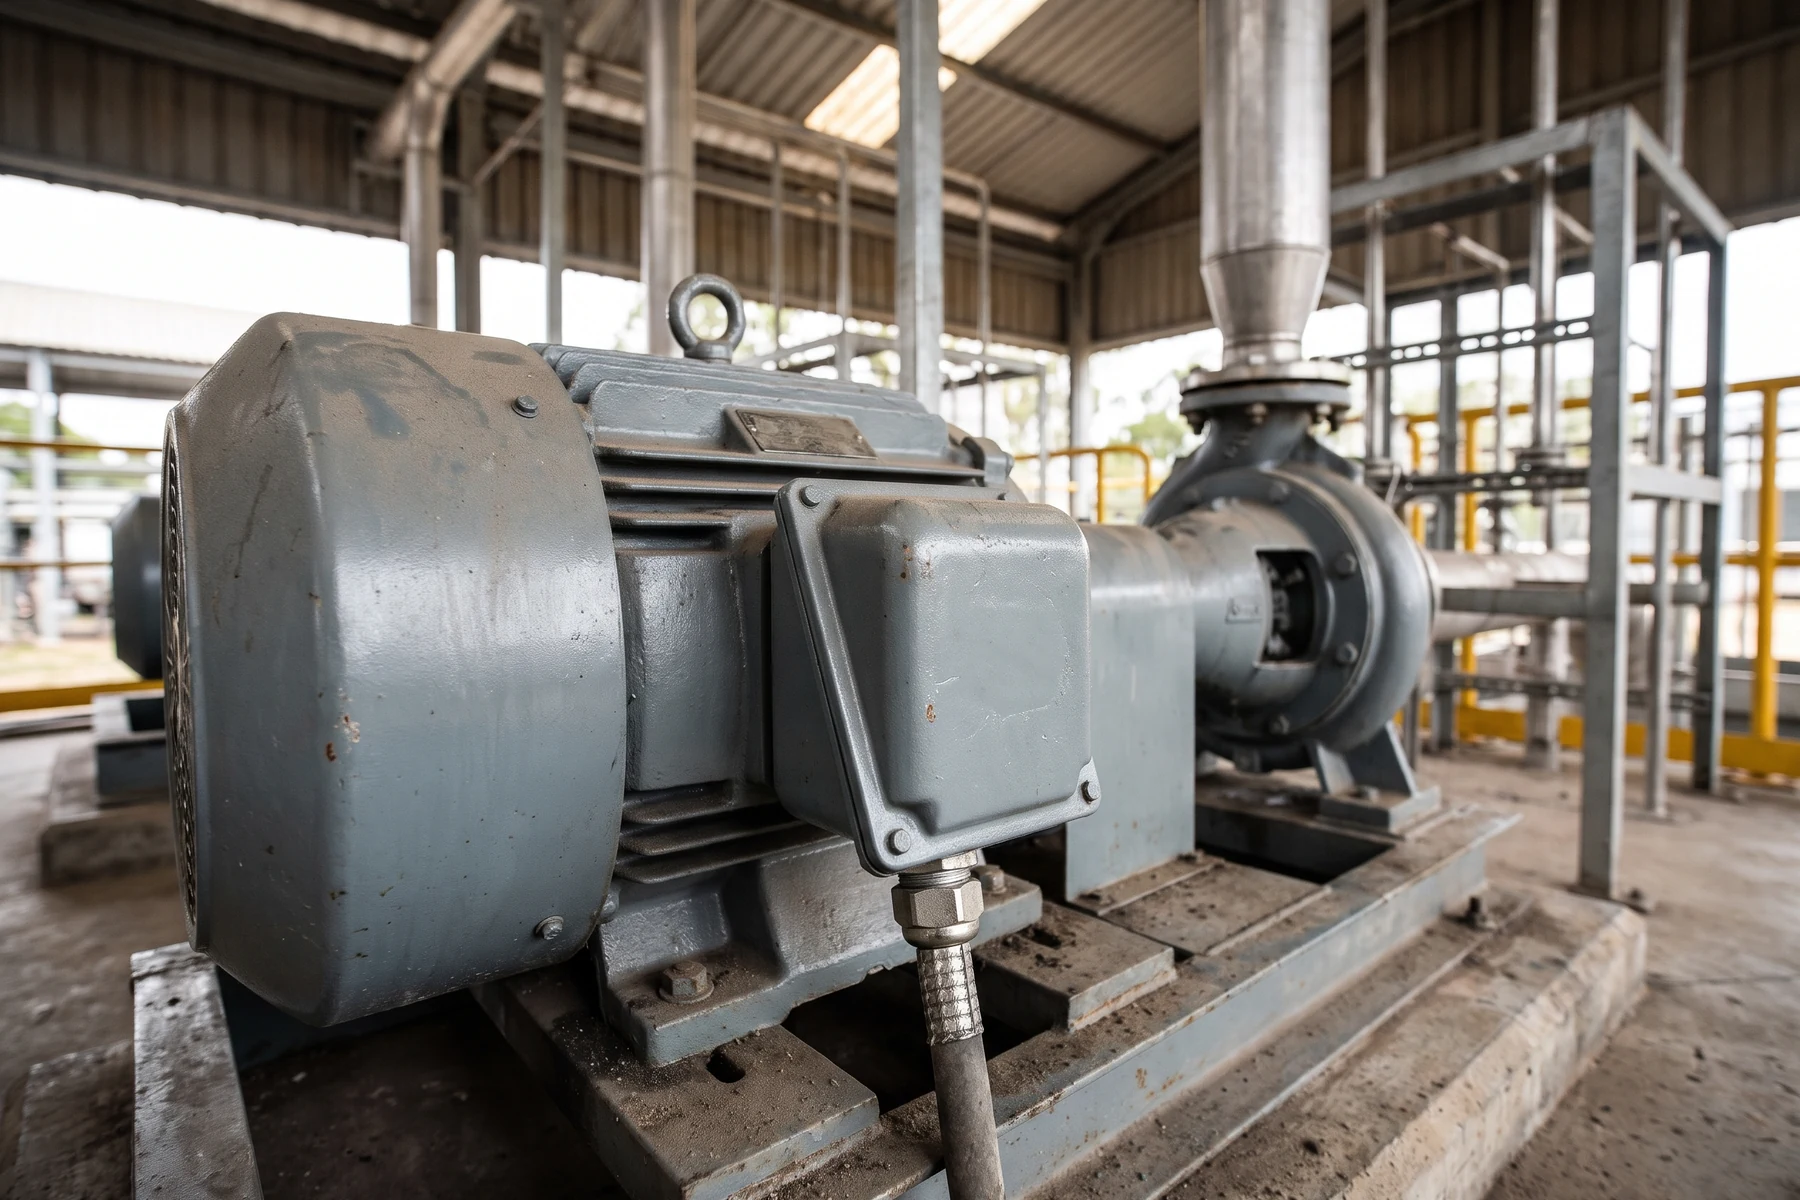
Walk through the pump house of a refinery and you will find two very different-looking motors doing the same job. One is a heavy cast-iron flameproof motor with a thick terminal box bolted shut. The other looks almost like an ordinary industrial motor — but its nameplate says Ex e or Ex eb. That is an increased safety motor, and choosing between the two is one of the most common questions we get from engineers in Refineries, Chemical Plants, Pharmaceutical Plants and Paint Shops. Here is how increased safety works, where it is allowed, and when flameproof is still the better answer.
1. What “Increased Safety” Means
A flameproof (Ex d) motor assumes that gas will get inside and may ignite — so the enclosure is built strong enough to contain the explosion and cool the escaping gases through precision flame paths. An increased safety (Ex e) motor takes the opposite approach: it is designed so that nothing inside it ever becomes an ignition source in the first place. No sparks, no arcs and no surface hot enough to ignite the surrounding gas — not in normal running, and not during the faults it is designed to withstand.
Because a squirrel cage induction motor has no brushes, commutator or switching contacts, it is a natural fit for this method. The design standard is IEC 60079-7 (IS/IEC 60079-7 in India).
2. How an Ex e Motor Is Built Differently
- Enhanced winding insulation and impregnation, so the winding is far less likely to fail into a spark.
- Larger creepage and clearance distances at every live part, especially in the terminal box.
- Secure, anti-loosening terminals — a loose connection is a classic ignition source, so Ex e terminals are designed not to work loose under vibration.
- Controlled rotor–stator air gap and rotor construction, so the rotor cannot rub or spark.
- Strict temperature limits on every surface, inside and out, including during a stalled (locked-rotor) condition — this is the key difference, explained in section 4.
- Ingress protection of at least IP54 (IP55 is typical), so dust and moisture cannot compromise the insulation.
The result is a motor that is noticeably lighter and simpler than an equivalent flameproof unit — no heavy flame-path machining, and an ordinary-looking terminal box.
3. Ex eb vs Ex ec — the Newer Markings
Since the 2015 edition of IEC 60079-7, increased safety comes in two levels of protection. You will see both on current CG nameplates:
| Marking | Equipment protection level | Permitted zones | Notes |
|---|---|---|---|
| Ex eb (formerly Ex e) | Gb — high protection | Zone 1 and Zone 2 | The classic “increased safety” motor |
| Ex ec | Gc — enhanced protection | Zone 2 only | Replaces the older non-sparking Ex nA motor |
A typical full marking reads Ex eb IIC T3 Gb: increased safety, suitable for gas group IIC, temperature class T3 (maximum surface temperature 200°C), equipment protection level Gb. Our guide to gas groups IIA, IIB and IIC explains each part of that code.
4. The tE Time — the Number That Matters Most
Every Ex e motor nameplate carries two figures you will not find on an ordinary motor:
- tE time (seconds) — how long the winding takes to heat from its normal running temperature to the limiting temperature for its temperature class if the rotor locks while the motor is energised.
- IA/IN — the ratio of starting (locked-rotor) current to rated current.
The protection rule is simple and non-negotiable: the motor’s overload protection must trip a stalled motor within its tE time. In practice that means checking the overload relay’s trip curve at the nameplate IA/IN ratio and confirming the trip time is shorter than tE. A standard relay set correctly is often fine, but a slow (Class 20 or 30) relay chosen for a long run-up may not be — which brings us to the main limitation of Ex e.
5. Ex e vs Flameproof Ex d — Side by Side
| Increased safety (Ex eb) | Flameproof (Ex d / Ex db) | |
|---|---|---|
| Principle | Prevents any ignition source | Contains an internal explosion |
| Zones | Zone 1 and 2 | Zone 1 and 2 |
| Weight and size | Lighter, close to a standard motor | Heavier, robust cast-iron enclosure |
| Cost | Usually lower, especially at larger ratings | Usually higher |
| Heavy or long starts | Limited by tE time | Much more tolerant |
| VFD operation | Only if certified for that motor–drive combination | Common, with thermistor protection |
| Terminal box | Ex e box, easy to wire and inspect | Flameproof box, flame paths must not be damaged |
| Maintenance | Simpler — no flame paths | Flame-path surfaces must be protected and inspected |
6. When to Choose Ex e — and When Not To
Ex e is usually the better choice for centrifugal pumps, fans, blowers, agitators and compressors that start quickly on direct-on-line or star-delta starters, in Zone 1 or Zone 2. These make up the bulk of motors in Refineries, Chemical Plants, Pharmaceutical Plants and Paint Shops. For Zone 2-only areas, an Ex ec motor is the economical option.
Choose flameproof (Ex d) instead when:
- The load has a long or heavy start — large fans with high inertia, crushers, loaded conveyors — where run-up time approaches the tE time.
- The motor will run on a variable frequency drive and no certified Ex e motor-and-drive combination is available. See our note on using VFDs with flameproof motors.
- Frequent starts and stops are expected, since repeated starting heats the winding towards its limit.
- The site’s own standards or the client’s specification call for Ex d.
For large HV drives where neither fits well, a pressurised (Ex p) motor — kept at positive pressure with clean air or inert gas — is the third option.
7. Certification in India
Any motor installed in a classified hazardous area in India needs approval from PESO (Petroleum and Explosives Safety Organisation), in addition to its IEC-based test certificate. Always ask for the PESO approval and the test certificate together, and check that the marking on the certificate matches the nameplate and your area classification. Our ATEX, IECEx and PESO guide covers what each certificate proves.
8. Maintenance and Rewinding
- Keep terminal connections tight and the terminal box gasket intact — these are the most common faults found on inspection.
- Never drill extra cable entries or fit uncertified cable glands; use Ex e glands of the correct size.
- Do not change the overload relay for one with a slower trip class without rechecking it against tE.
- Rewinding must preserve the certification. A rewind changes the winding’s thermal behaviour and therefore its tE time. Have Ex e motors repaired only by a repairer qualified for hazardous-area equipment, or replace the motor — see rewinding vs replacement.
9. Quick Checklist
- Zone 1 → Ex eb or Ex d. Zone 2 → Ex ec, Ex eb or Ex d.
- Gas group and temperature class on the nameplate cover your area’s gas
- Run-up time comfortably shorter than tE; overload relay trips within tE at IA/IN
- Fixed-speed duty, or a certified motor-and-drive combination for VFD use
- PESO approval and test certificate supplied, matching the nameplate
- Ex e cable glands and a sealed terminal box at installation
Bombay Engineering Syndicate supplies CG Power’s complete hazardous-area range: increased safety Ex e LV motors, Ex e HV motors, Ex ec motors for Zone 2 and flameproof motors. Not sure which protection method your application needs? Send us the area classification, the gas, the load and the starting method, and we will recommend the right motor.